


 15 mins
Jun 26, 2026

A camera on a production line can tell you that a part looks different.
The harder engineering problem is deciding whether that difference matters, why it happened, and what the factory should do next.
That problem is getting more attention in 2026.
In fact, IMTS 2026, which took place on September 14–19 in Chicago, introduced its first Industrial AI Arena, while its vision technology coverage included metrology, optical inspection, inline 3D scanning, and vision-guided automation.
These applications raise a bigger question for manufacturers.
And this blog covers exactly that.
Manufacturing computer vision is moving from fixed inspection rules.
With AI models, it can now detect complex defects, identify anomalies, measure components, and handle product variation that is difficult to capture through predefined conditions.
NIST’s 2026 Roadmap on AI and Machine Learning for Smart Manufacturing puts this in a broader context.
It connects advanced sensing and perception with quality assurance, process control, robotics, digital twins, and industrial data. It also highlights interoperability and data management as important requirements for getting AI systems to work across manufacturing environments.
For computer vision, this means the image is only one part of the input. A production system may combine visual data with machine signals, process parameters, quality records, and production history before deciding what happens next.
The focus is therefore moving from detecting a problem to reliably interpreting it within the production process.
The right approach depends on the production problem.
| Manufacturing Problem | Computer Vision / Imaging Approach | What the System Detects | Production Decision |
|---|---|---|---|
| Surface Scratches & Cracks | Segmentation, classification, anomaly detection | Defect type, severity, and location | Accept, reject, or send for rework |
| Missing Components | Object detection | Component presence and position | Pass/fail or assembly alert |
| Wrong Components | Object detection + classification | Component identity and placement | Stop, reject, or correct assembly |
| Dimensional Deviations | 2D/3D vision, metrology | Geometry and tolerance deviation | Accept/reject against specification |
| Incorrect Labels | OCR + visual inspection | Text, barcode, and label placement | Verify traceability |
| Packaging Defects | Detection + OCR | Seal, label, print, and package condition | Approve/reject package |
| Weld Anomalies | Segmentation + classification | Weld geometry and visible defects | Flag for inspection or rework |
| Part Identification | OCR + visual recognition | SKU, serial number, or lot | Track part through production |
| Process Deviations | Video analytics + anomaly detection | Unexpected movement or process behavior | Alert operator or intervene |
| Robot Guidance | Detection + pose estimation + 3D vision | Part position and orientation | Guide robot movement |
| Worker Safety | Object detection + video analytics | PPE, restricted-area entry, and unsafe events | Trigger safety response |
| Internal Defects | X-ray, CT, and other NDT imaging | Porosity, inclusions, voids, and internal geometry | Qualify or reject component |
| Surface & Material Characteristics | Thermal or hyperspectral imaging | Properties invisible to standard RGB cameras | Identify material or process anomaly |
| Machine & Process Condition | Vision + machine/process data | Visual signs of tool wear or process change | Trigger maintenance or process review |
Here’s how today’s most advanced factories are embedding visual intelligence into their operations:
Industrial-grade cameras (RGB, thermal, line-scan) are deployed on production lines, workstations, and in warehouses.
These cameras capture high-resolution images at high speeds, even in challenging conditions like low light or fast motion.
Raw visual data is often noisy or inconsistent due to real-world factory conditions like varying lighting, vibration, oil smudges, or moving parts.
Preprocessing ensures data quality before AI models analyze it.
Here, computer vision algorithms identify regions of interest (ROIs) even if the orientation or placement varies slightly.
For example, in a gear assembly line, the system will isolate the gear housing, locate the mounting holes, and check whether the fasteners are present and aligned correctly.
Algorithms like YOLO (You Only Look Once) and Mask R-CNN ensure even the smallest anomalies or missing components don’t slip through.

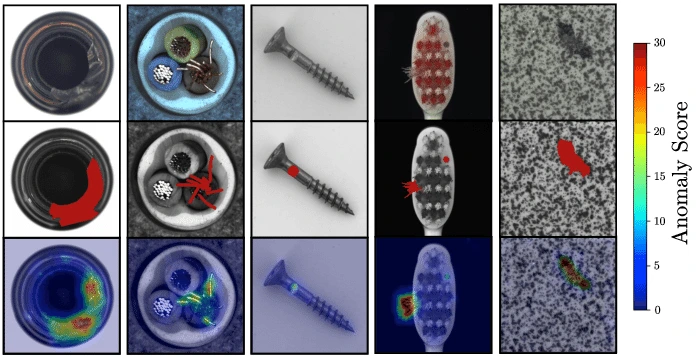
Computer vision detects surface scratches, dents, misalignments, soldering issues, or packaging defects — often at a pixel-level sensitivity beyond human vision.
Here’s an example where,
Human actions (e.g., assembly motions, lifting, tool usage) are tracked to assess workflow compliance, ergonomics, or unsafe behavior.

Once defects, anomalies, or unsafe behavior are detected, signals are pushed to manufacturing execution systems (MES), programmable logic controllers (PLCs), or SCADA platforms.
For example, if a surface defect is found on an automotive panel, the system automatically pushes the part to a rework station and logs it against the part’s serial ID for traceability.
This is the final layer.
Operators or QC inspectors validate edge cases missed or wrongly flagged by the AI. These are looped back into the training data for model retraining via an MLOps pipeline.
Over time, the model adapts to production changes like new materials, lighting shifts, or part geometry tweaks — without needing manual reconfiguration.
Let’s look at how computer vision in manufacturing is being executed by global leaders to bring efficiency value across the shop floor.
At BMW’s Regensburg plant, quality control has entered a new era. The automaker has implemented a fully automated, AI-powered visual inspection system for painted vehicle surfaces, right on the production line.

Using deflectometry, geometric light patterns are projected onto the vehicle surface and captured by high-resolution cameras. AI-controlled robotic arms then analyze the reflections to detect even the smallest imperfections in paintwork — scratches, dents, uneven coatings — and mark them for post-processing.
With computer vision embedded into their MES (Manufacturing Execution System), BMW is ensuring every car that leaves the plant meets its precision-crafted expectations.
Tata Steel has turned to computer vision to enhance worker safety.
Using smart surveillance systems powered by AI, as part of an enterprise security camera system, the company monitors real-time PPE (Personal Protective Equipment) compliance. The system automatically detects whether employees are wearing helmets, gloves, safety goggles, and vests, flagging any violations instantly.

By combining video analytics with workplace IoT infrastructure, Tata Steel is moving from reactive incident response to proactive risk mitigation.
Foxconn, the electronics manufacturing giant, has taken a bold step forward with its AI-based visual inspection system — NXVAE.
What’s different here? It’s unsupervised learning. NXVAE identifies anomalies on its own, no need for thousands of labeled defect images. This means faster deployment and better scalability across new product lines.
Additionally, Foxconn has partnered with Siemens to deploy digital twin models of entire production lines using real-world sensor data and computer vision insights to simulate, stress-test, and optimize workflows long before any physical build-out.
Amazon’s fulfillment centers are the poster child of modern logistics, and computer vision is central to that transformation.
Robotic systems, like Vulcan, use visual and tactile sensors to navigate, sort, and retrieve inventory with precision that mimics human dexterity. Overhead cameras and shelf scanners feed into a real-time inventory management system, which enables dynamic space optimization and faster order fulfillment.
Many facilities integrate industrial security camera systems to continuously monitor loading docks, storage aisles, and packing areas, supporting compliance, asset tracking, and worker safety.

The result? Reduced human error, faster pick-and-pack cycles, and fully automated stock tracking, even during high-volume peaks like Prime Day.
Airbus is reimagining aircraft assembly with help from Accenture and a suite of AI-powered vision technologies.
By integrating computer vision into the final assembly process, Airbus is enabling real-time part tracking, human-robot collaboration, and automated inspection of complex components like fuselage joints and engine mounts.

It’s a prime example of Industry 4.0 in action, where AI-driven feedback loops accelerate throughput while maintaining exacting aerospace standards.
Novo Nordisk employs computer vision combined with machine learning to automate key tasks on manufacturing lines, such as cartridge counting and anomaly detection.
This automation reduces manual labor and enhances the accuracy and efficiency of their production processes.
Manufacturers deploy computer vision through specialized solution categories designed to address quality, safety, automation, and operational efficiency challenges.
Each solution integrates hardware, AI models, and production systems to support scalable industrial deployment.
End-to-end inspection systems designed to detect defects, validate product quality, and enforce production standards across manufacturing lines. These platforms operate continuously and replace manual inspection processes with consistent, data-driven quality validation.
Components typically include:
→ Industrial cameras for high-resolution image capture
→ AI inference engines for defect detection and classification
→ Inspection dashboards for real-time monitoring
→ Production integration modules for automated response
→ Quality data storage for traceability and compliance
For more insights, read our blog on: AI for Manufacturing Quality Control
Vision-enabled robotic systems that combine machine vision with industrial robotics to automate handling, assembly, and inspection tasks. These systems allow robots to recognize objects, adapt to variations, and make real-time positioning decisions.
Typical capabilities include:
→ Object detection for pick-and-place operations
→ Assembly guidance for component positioning
→ Adaptive handling for variable materials
→ Precision alignment and placement verification
→ Automated inspection during robotic workflows
AI-powered monitoring solutions designed to improve workplace safety and ensure compliance with industrial regulations. These systems continuously analyze video streams to detect safety risks and operational hazards.
Core functionalities include:
→ Personal protective equipment detection
→ Restricted zone monitoring
→ Worker movement and behavior analysis
→ Hazard identification and incident alerts
→ Safety compliance reporting
Computer vision solutions that analyze production activities to identify inefficiencies, monitor workflows, and improve operational performance. These platforms convert visual production data into actionable insights.
Key capabilities include:
→ Production flow analysis
→ Bottleneck detection
→ Machine utilization monitoring
→ Cycle time measurement
→ Process deviation detection
Visual monitoring solutions that detect early signs of equipment wear, component damage, or abnormal machine behavior. These systems identify issues before they cause production failures.
Typical monitoring capabilities include:
→ Equipment surface condition monitoring
→ Leak detection and fluid monitoring
→ Vibration pattern observation
→ Component wear detection
→ Abnormal movement analysis
For more insights, read our articles on predictive maintenance:
Computer vision solutions designed to automate material tracking, inventory management, and warehouse operations across manufacturing facilities and distribution centers.
Common capabilities include:
→ Automated inventory counting
→ Material identification and tracking
→ Package sorting and routing
→ Shipment verification
→ Warehouse navigation support
Specialized vision systems that ensure packaging accuracy, labeling compliance, and product integrity before distribution. These solutions are widely used in regulated industries.
Key functions include:
→ Label placement verification
→ Barcode and serial number validation
→ Seal integrity inspection
→ Expiration date verification
→ Regulatory marking validation

Yes. You can integrate computer vision in manufacturing facilities without replacing entire production systems.
Cameras and sensors can be installed on existing equipment with minimal disruption. Mounting systems and industrial enclosures support harsh production environments.
Middleware and industrial communication protocols enable integration with older production systems.
Manufacturers typically start with a controlled pilot project to validate performance and ROI before full-scale deployment.
Successful integration requires:
→ Reliable network connectivity
→ Adequate processing capacity
→ Data storage infrastructure
→ Process workflow alignment
Operators must understand system outputs and workflows to ensure adoption and operational success.
Computer vision in manufacturing continues to evolve rapidly.
Modern computer vision systems increasingly process images directly on production equipment instead of sending data to centralized servers.
Edge processing enables real-time inspection, faster decision-making, and reduced network dependency.
Manufacturing vision systems now rely heavily on deep learning models rather than rule-based image processing.
These models detect complex defect patterns, adapt to product variations, and improve accuracy over time.
A major challenge in manufacturing is limited defect data. Generative AI now helps create synthetic images of defects to train models faster and improve detection accuracy.
This enables faster deployment of vision systems, improved detection of rare defects, reduced data labeling effort, and better model performance in new production environments.
Manufacturers are increasingly adopting 3D vision systems that capture depth and spatial information instead of relying only on 2D images.
These systems support precise dimensional measurement, robotic guidance and automation, complex assembly validation, and inspection of irregular or reflective surfaces.
Computer vision is becoming the foundation of intelligent robotics in manufacturing environments. Vision-guided robots can identify objects, adapt to changes, and perform tasks with minimal human intervention.
This supports autonomous inspection systems, flexible production lines, adaptive assembly operations, and human-machine collaboration.
Modern manufacturing systems combine visual data with information from other sensors such as thermal imaging, vibration monitoring, and IoT devices.
This creates a more complete understanding of production environments.
Computer vision increasingly feeds real-time production data into digital twin environments and smart factory platforms. These systems simulate production processes and help manufacturers optimize operations before implementing changes.
This enables predictive process optimization, production scenario testing, real-time performance monitoring, and continuous improvement initiatives.
Manufacturers are moving from isolated AI pilots to enterprise-wide computer vision deployment across multiple plants. This allows standardized inspection processes, centralized model management, and consistent quality control globally.
The industrial AI market is growing rapidly as manufacturers scale AI-driven operations across production environments.
For more insights related to manufacturing AI, read our articles:

Computer vision delivers strong value in industries with high precision requirements, complex assembly processes, and strict regulatory standards. Automotive, aerospace, electronics, pharmaceuticals, food processing, and industrial equipment manufacturing see the highest adoption. These sectors rely on visual inspection, traceability, and process validation where consistent quality and compliance directly impact revenue and safety.
Implementation cost depends on production complexity, camera infrastructure, AI model development, and system integration requirements. Pilot deployments may range from tens of thousands of dollars, while enterprise-scale deployments can reach several hundred thousand or more. Most manufacturers evaluate cost based on expected savings from reduced defects, lower rework, and improved throughput rather than initial investment alone.
Manufacturers typically observe measurable ROI within 6–18 months depending on use case complexity and production scale. High-volume production environments achieve faster returns due to reduced scrap, improved yield, and lower inspection costs. ROI also increases over time as systems improve through continuous learning.
The amount of data required depends on the use case and model type. Traditional deep learning models require labeled production images, while newer approaches such as anomaly detection and self-supervised learning require fewer labeled examples. Many implementations begin with limited datasets and expand model accuracy through ongoing production data.
Common challenges include inconsistent lighting conditions, product variability, data labeling requirements, integration with existing systems, and change management within operations teams. Successful deployment requires careful planning, pilot testing, and collaboration between manufacturing and AI engineering teams.
 15 mins
 28 mins
"*" indicates required fields

5432 Geary Blvd, Unit #527 San Francisco, CA 94121 United States
320 Decker Drive Irving, TX 75062 United States

6d-7398 Yonge St,1318 Thornhill, Ontario, Canada, L4J8J2
71-75 Shelton Street, Covent Garden, London, United Kingdom, WC2H 9JQ

Hohrainstrasse 16, 79787 Lauchringen, Germany

12, Zugerstrasse 32, 6341 Baar, Switzerland

5th floor, Bloukrans Building, Lynnwood Road, Pretoria, Gauteng, 0081, South Africa

12th & 13th Floor, B Square-1, Bopal – Ambli Road, Ahmedabad – 380054
B/305A, 3rd Floor, Kanakia Wallstreet, Andheri (East), Mumbai, India




 Talk to Our
Consultants
 Chat with
Our Experts
 Write us
an Email